The Challenge
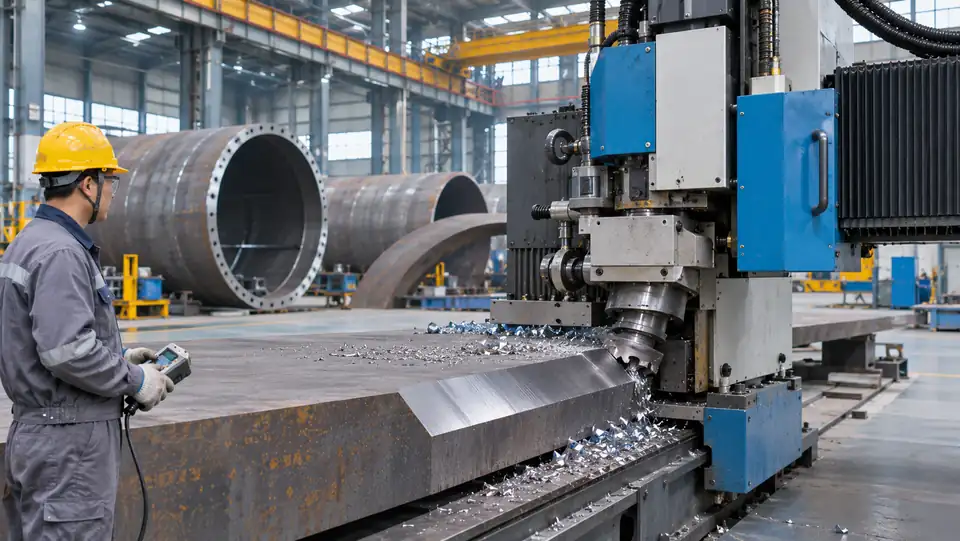
On thick shell plate a plain V-groove opens up very wide, which multiplies the filler metal and welding hours. U and J grooves solve that but are hard to produce accurately with a torch, and alloy steels need any heat-affected material removed before welding.
Our Solution
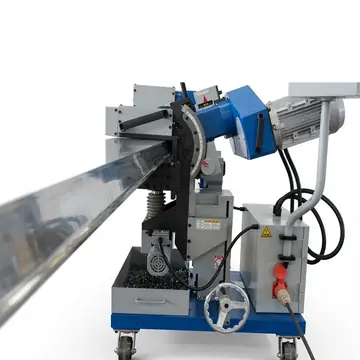
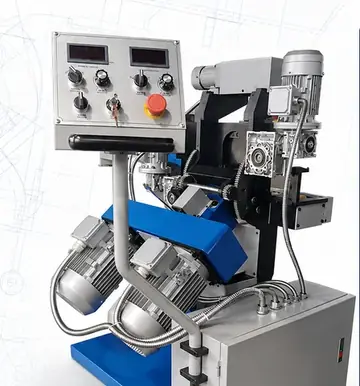
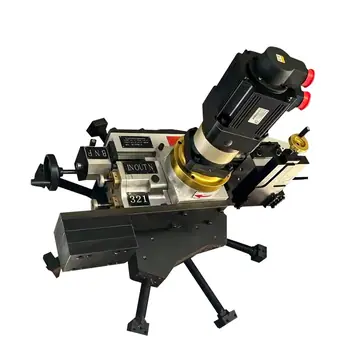
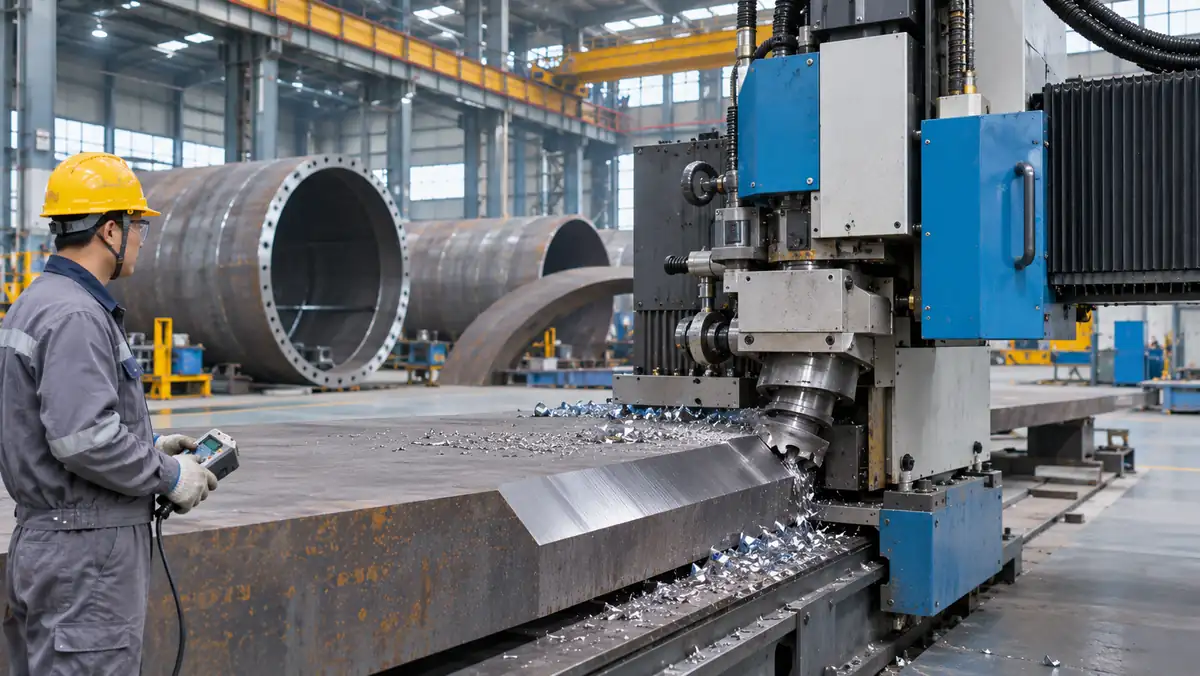
The GMMA-100U mills the U-groove root radius directly with a Ø100 mm cutter, while the GMMA-100L handles J-preps and deep V-bevels up to 100 mm wide on 8–100 mm plate. Both cut cold, so there is no heat-affected zone on Cr-Mo material. Nozzle flanges are faced afterwards with a TFS-I1000.
Workflow
- Plates are laid out and the joint geometry confirmed against the WPS
- Root radius and groove are milled in several passes
- Bevel angle and land are checked with gauges at intervals
- Shells are rolled and longitudinal seams welded
- Nozzle flange faces are machined to finish after welding
Result
Grooves with consistent root radius and land are produced straight from the machine, and welders deposit less filler on each seam than with an equivalent V-groove.