The Challenge
Hull blocks use many double-sided K and X joints. Beveling one side, then lifting and flipping a 10 m plate to bevel the other, ties up the overhead crane and slows the whole panel line.
Our Solution
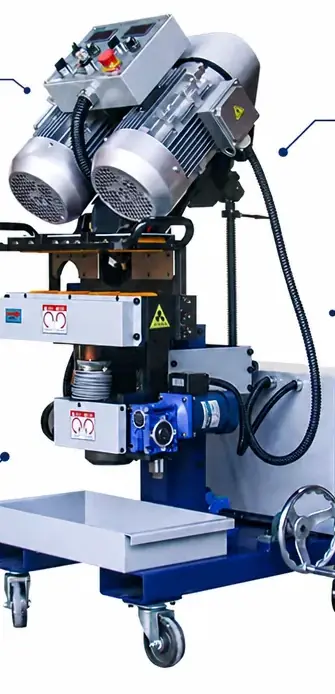
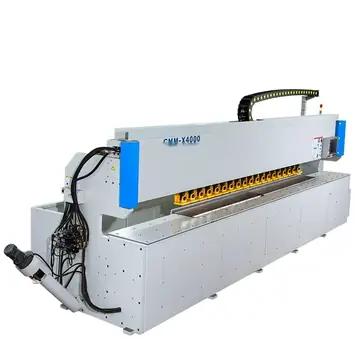
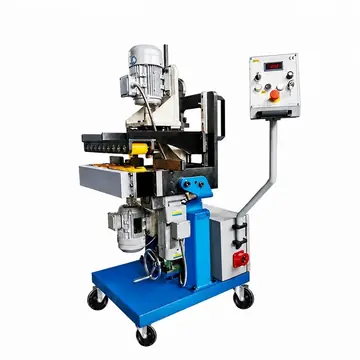
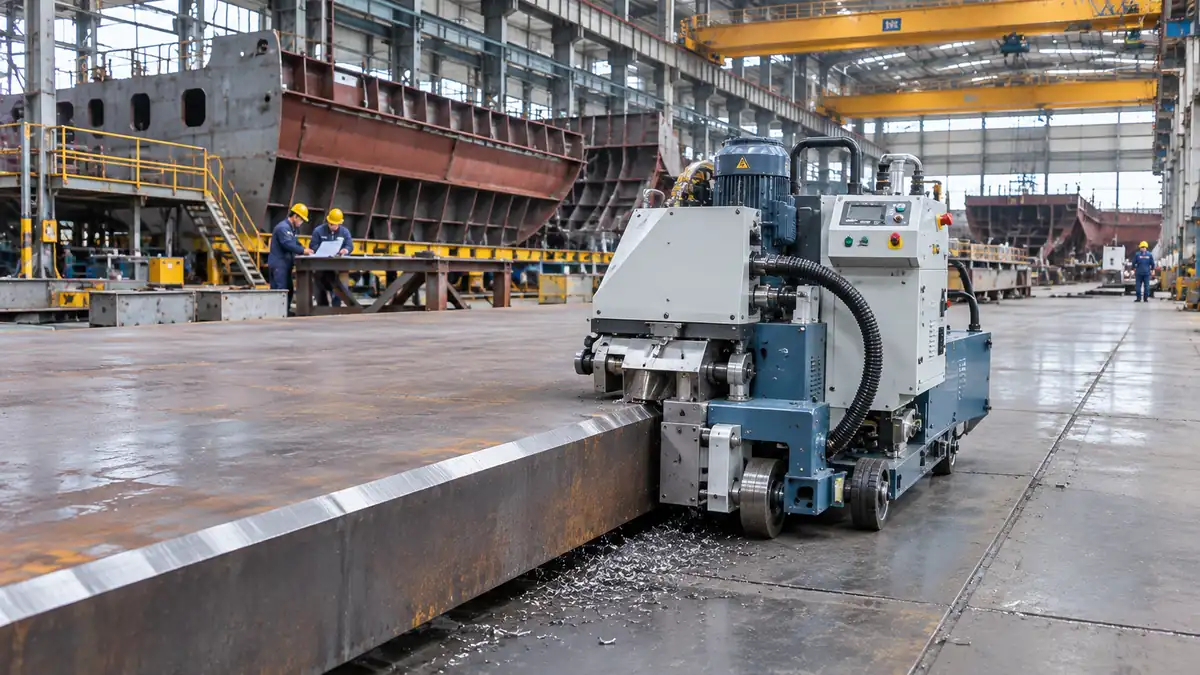
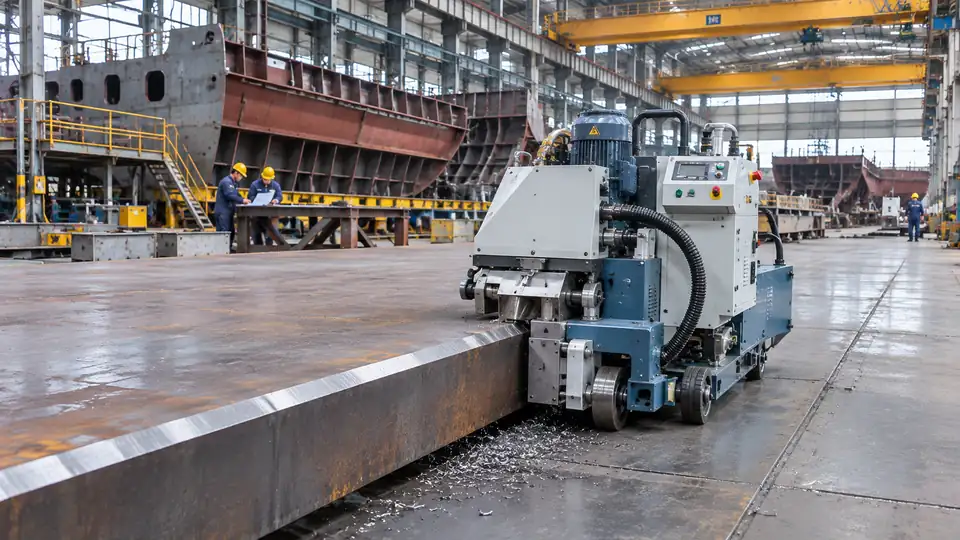
Walking GMM-80R machines run along the plate edge on the panel line itself. Their turnable head bevels the top face, then the underside, without moving the plate. Long, straight edges that repeat across many blocks go to a TMM-3000 CNC edge miller with two heads, so both sides are cut in one programmed cycle. A GCM-R3AR rounds free edges to R2 before blasting and painting.
Workflow
- Plates arrive from cutting with edges marked by joint type
- K/X edges on long plates are milled on the TMM-3000 in one cycle
- Remaining edges are beveled in place with GMM-80R walking machines
- Free edges are rounded R2 with the GCM-R3AR
- Plates go to blasting and priming
Result
Double-sided joints are prepared without crane lifts to turn the plate. Milled bevels need no grinding before welding, and rounded free edges meet the coating specification for edge preparation.