The Challenge
Tower shells are welded with submerged-arc welding, which needs uniform X or K preps along every longitudinal seam. After the flange is welded to the end can, welding distortion can take the flange out of flatness tolerance.
Our Solution
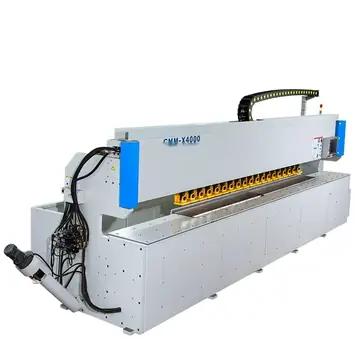
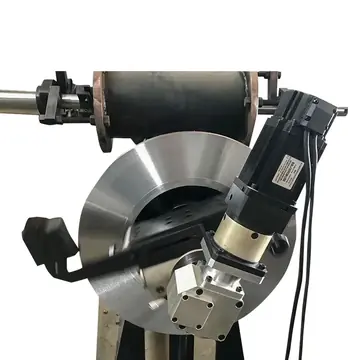
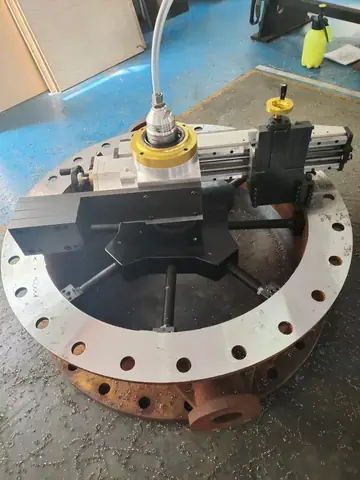
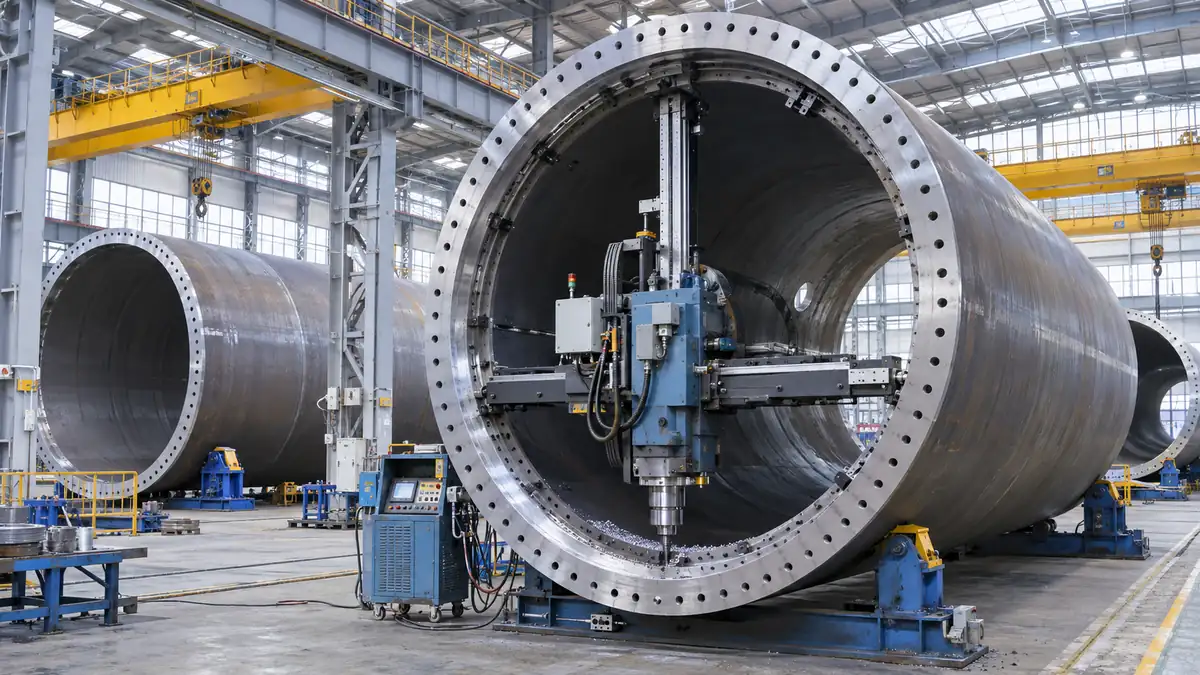
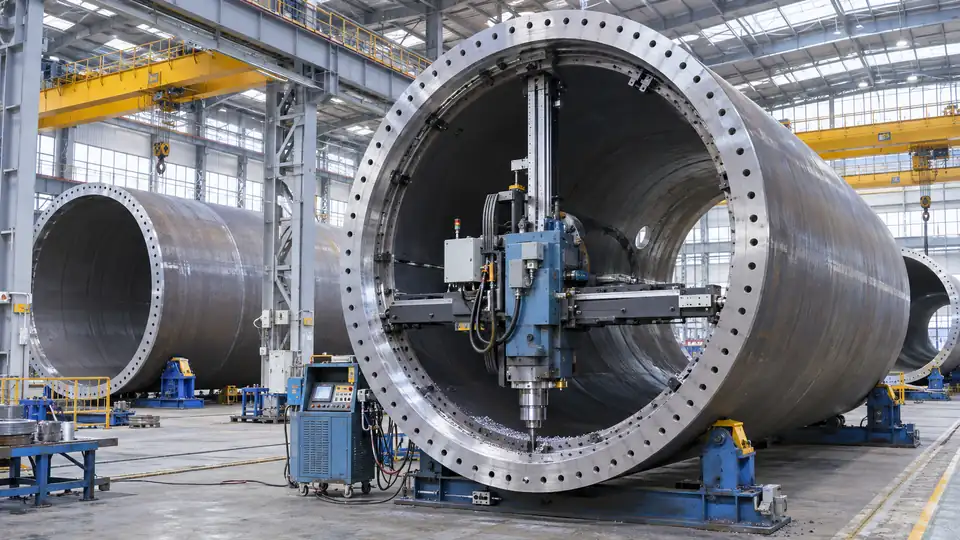
Shell plates are beveled on a TMM-3000 with both heads cutting the upper and lower bevels in one cycle. After welding, a TFP-3000 is mounted inside the tower flange to skim the face back to flatness, without moving the section to a vertical lathe.
Workflow
- Mill X/K bevels on shell plates
- Roll cans and weld longitudinal seams
- Fit and weld the flange to the end can
- Mount the TFP-3000 and skim the flange face
- Check flatness across the full diameter
Result
Uniform bevels for automatic welding, and tower flanges brought back to flatness in place.